Heat resistant rubber conveyor belts are essential components in industries where materials are subjected to high temperatures. These belts ensure efficient material handling without compromising the integrity of the belt or the safety of the operations. Understanding the various aspects of heat resistant conveyor belts, such as their construction, material properties, and applications, can help industries make informed decisions to enhance their operational efficiency.
Understanding Heat Resistant Conveyor Belts
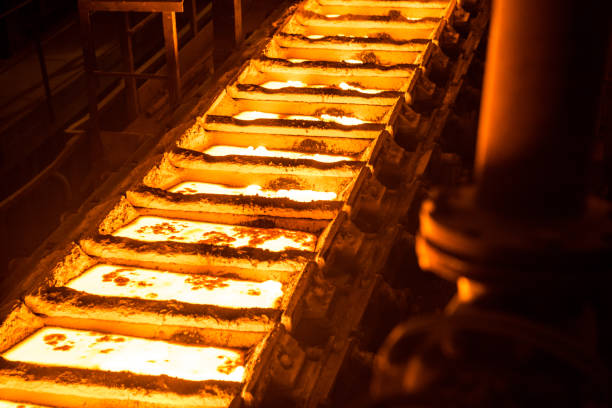
Heat resistant conveyor belts are designed to transport materials that are heated up to 250?C or even higher. They are manufactured using specially designed rubber compounds that provide excellent heat resistance and durability. Industries such as steel, cement, and chemical processing frequently rely on heat resistant conveyor belts to maintain productivity.
Key Features
- High-temperature resistance up to 400?C.
- Durability under thermal stress.
- Resistance to abrasion and wear.
- Flexibility to handle various materials.
- Long service life and reduced maintenance costs.
Applications Across Industries
Industries that process high-temperature materials benefit significantly from using heat resistant conveyor belt materials. These belts are crucial in operations where maintaining the integrity of the material and the conveyor system is paramount.
Common Industrial Applications
- Steel Manufacturing: Conveyor belts designed for high temperatures are used in the transportation of sinter, coke, and other hot materials.
- Cement Industry: Used for transporting clinker, a crucial component in cement production.
- Chemical Processing: Essential for handling chemicals that are processed at elevated temperatures.
- Power Plants: Employed in the handling of ash and other by-products of combustion.
Choosing the Right Heat Resistant Conveyor Belt
When selecting a heat resistant conveyor belt manufacturer, it is vital to consider the specific needs of the operation. Factors such as temperature range, material type, and environmental conditions play a crucial role in determining the appropriate belt type.
Selection Criteria
- Temperature Range: Ensure the belt can withstand the maximum temperatures expected in the operation.
- Material Composition: Choose a belt made from materials that will not degrade under thermal stress.
- Durability: Consider the operational lifespan and maintenance requirements of the belt.
- Cost-effectiveness: Balance the initial investment with long-term operational savings.
Advancements in Technology
Recent advancements in the development of high temperature conveyor belts have led to improved performance and reliability. Innovations in rubber compounds and belt structures have resulted in products that can endure even higher temperature ranges while maintaining flexibility and strength.
Conclusion
For industries that deal with high-temperature materials, investing in a reliable heat resistant belt is crucial. By understanding the specific requirements and applications, industries can select the right heat resistant rubber conveyor belt that will enhance productivity, safety, and cost-effectiveness. As technology evolves, the capabilities of heat conveyor belts continue to expand, offering more options tailored to specific industrial needs.
About the Author